10 Lost Wax Casting Tips for Global Buyers

Time:2026-10-07 Author:Aria
0%

Buying Lost wax casting components across borders can look simple on a drawing. In practice, small decisions often create expensive surprises. Wax pattern quality, ceramic shell strength, alloy selection, machining allowance, and inspection records all affect the final part. A polished sample may hide weak process control. That matters.

John Campbell, a respected casting researcher and author of Castings, wrote, “The quality of a casting is determined by the quality of the liquid metal.” His observation remains highly practical for global buyers. A supplier may offer an attractive price, but the real question is process stability. Can the foundry control melting temperature, pouring conditions, shell drying, and shrinkage during repeated production? Ask for evidence, not confident promises.

This guide, “10 Lost Wax Casting Tips for Global Buyers,” focuses on those purchasing details. It considers drawings, tolerances, material certificates, sample approval, surface defects, packaging, lead times, and communication. It also recognizes an uncomfortable truth: no supplier or buyer controls every variable perfectly. Weather, transport delays, tooling revisions, and unclear specifications can still interfere. Good planning reduces risk, but it does not remove it.

Look closely.

Experienced buyers compare inspection methods, not only unit prices. They request clear acceptance criteria before production begins. They also leave room for improvement after the first batch. That step is often neglected. A practical sourcing decision combines technical proof, transparent communication, and realistic expectations.
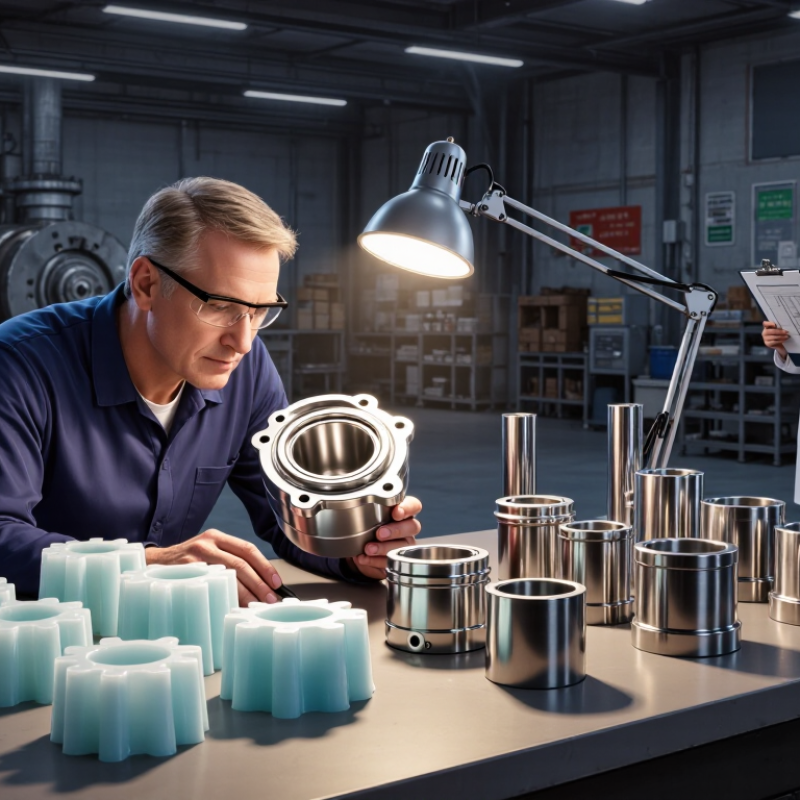
10 Lost Wax Casting Tips for Global Buyers

Understanding the Lost Wax Casting Process and Its Key Quality Factors

Lost Wax Casting Tips for Global Buyers

Understanding the Lost Wax Casting Process and Its Key Quality Factors

The World Foundry Organization’s 2023 World Casting Census reports roughly 100 million tonnes of global castings in 2022. That scale hides variation. Lost wax casting starts with a precise wax pattern, followed by ceramic shell building, dewaxing, metal pouring, cutting, heat treatment, and inspection. Check wax dimensions before shell production. Confirm shrinkage allowances with actual trial data. Inspect the shell for cracks, thin areas, and trapped moisture. Record slurry viscosity and drying conditions. Small omissions become expensive defects.

During pouring, verify alloy chemistry with a material certificate and heat number. Control temperature, fill time, and gating design. Do not judge internal soundness by appearance alone. Radiographic or penetrant testing may be necessary, depending on service risk. Use ISO 8062-3 tolerances only after confirming the supplier’s achievable process capability. A tighter tolerance can increase machining, scrap, and lead time. It is not automatically better. Request a first-article report, dimensional records, and heat-treatment results. Keep every result traceable to a batch.

A useful admission: a perfect sample does not prove stable production. Ask for process capability data from repeated lots, not one attractive part. Review surface roughness, wall thickness, and datum methods together. Packaging also matters; thin investment castings can bend during overseas transport. One overlooked detail is humidity control. Require dry separators and corrosion protection when the alloy needs them. Independent inspection can reduce uncertainty, but it cannot repair unclear drawings or missing acceptance criteria.

Defining Alloy, Dimensions, Tolerances, and Surface Finish Requirements

Global buyers should define the alloy before requesting an investment casting quotation. State the complete grade, applicable standard, heat-treatment condition, and required mechanical properties. “Stainless steel” is not enough. The 2023 World Casting Census reported global casting production above 100 million metric tonnes, showing how widely material specifications vary between supply regions. Ask for a material certificate, chemical analysis, and heat-treatment records. Small wording gaps can create large performance risks.

Tip: Send a dimensioned 3D model and a controlled drawing. Mark critical dimensions clearly. ISO 8062-3 provides casting tolerance grades, but general tolerances should not govern sealing faces, bearing seats, or assembly datums. Define measurement equipment, datum structure, and inspection temperature. A 0.2 mm tolerance may be realistic in one area and expensive in another. Buyers sometimes specify precision everywhere. That is usually wasteful.

Tip: Describe surface finish with measurable values, not appearance words. Specify roughness, such as Ra, inspection locations, and the acceptable visual condition. ASTM E125 can support visual comparison for certain surface indications, while roughness testing requires a calibrated instrument. Include requirements for flash removal, gate marks, pits, and shot-blast texture. Do not promise a flawless surface. Even experienced teams miss one hidden recess. Request sample approval, first-article inspection, and photographs of difficult areas before production. A short review prevents costly assumptions.

Evaluating Suppliers, Certifications, Samples, and Production Capabilities

Global buyers should evaluate lost wax casting suppliers through evidence, not polished websites. Ask for records covering wax injection, shell building, burnout, pouring, and finishing. A capable supplier can explain shell thickness and pouring temperature controls. Request recent inspection reports, material certificates, and equipment calibration records. Small gaps matter.

Check each certification’s scope, issuing body, validity, and production site. A certificate without matching scope proves little. Ask for a sample made with the same alloy, geometry, and surface finish as your order. Inspect thin walls, sharp corners, holes, and visible weld repairs. Request dimensional data from a coordinate measuring machine or calibrated gauges. An attractive sample may hide weak process control. I still treat perfect samples cautiously.

Production capability requires more than a machine list. Confirm monthly capacity, tooling resources, furnace size, inspection staff, and backup equipment. Ask how batches are identified from raw material to final packing. A pilot order can reveal actual yield, defect patterns, and lead times. Request one corrective-action report, even if the supplier says defects are rare. That answer may expose their honesty. Share drawings with revision numbers and written tolerances. Vague specifications create avoidable disputes. Some suppliers need reminders. That is not ideal. Regular technical reviews, retained samples, and documented approval points make cooperation more reliable.

Managing Tooling Costs, Minimum Orders, Lead Times, and Payment Terms

Before requesting a quote, separate tooling from each casting price. A wax injection die may cost more than expected, especially with complex cores or tight tolerances. Ask whether the quoted tooling includes design review, trial shots, and one correction round. Get ownership and storage terms in writing. I once saw a low unit price hide expensive mold modifications. That mistake delayed sampling by three weeks.

Minimum order quantities should match the process, not only your sales forecast. Small batches can carry high setup and furnace costs. Larger batches may reduce unit prices, but they can trap cash in slow-moving inventory. Request pricing at three volumes, such as 50, 200, and 1,000 pieces. Confirm acceptable scrap rates and whether mixed sizes count toward the minimum. The cheapest tier is not always the safest choice.

Build lead time around real production stages: approved drawings, tooling, wax patterns, ceramic shells, casting, finishing, inspection, and export packing. Ask for calendar days and milestone dates, not vague promises. Add buffer for sampling and customs. Payment terms also need detail. A practical structure may include a tooling deposit, production deposit, and balance after inspection. Define inspection evidence, currency, bank fees, and late-change charges. These terms protect both sides. Still, challenge the schedule: sea freight, rework, and holiday closures can disrupt a careful plan.

Inspecting Castings and Coordinating Global Packaging, Shipping, and Compliance

Lost wax castings need inspection before packaging, not after a container leaves port. Check critical dimensions against approved drawings, especially holes, threads, and mating surfaces. Examine thin sections for incomplete filling, cracks, and ceramic inclusions. Surface color can mislead. Use calibrated gauges and record results with photographs, heat numbers, and material certificates.

Packaging must protect both geometry and traceability. UNCTAD’s Review of Maritime Transport 2023 reports that ships carry over 80% of global merchandise trade by volume. Therefore, castings may face vibration, humidity, salt air, and repeated handling. Wrap clean parts with suitable corrosion protection, add separators, and immobilize heavy pieces inside reinforced cartons or crates. Include desiccant when moisture exposure is likely. Mark package weight and lifting points clearly. Small labels matter.

The World Bank’s Logistics Performance Index 2023 evaluates customs, infrastructure, shipment tracking, and timeliness. These factors should shape the shipping plan. Confirm the importer’s required HS classification, country-of-origin marking, packing list, commercial invoice, and inspection documents before dispatch. Requirements can differ by destination and product material. Ask the buyer to approve the document set. A perfect first shipment is unlikely. Even experienced teams miss a label or underestimate crate weight. Reviewing those failures openly improves the next order.

10 Lost Wax Casting Tips for Global Buyers

Inspecting castings and coordinating global packaging, shipping, and compliance

Approximate internal container volume helps buyers coordinate casting dimensions, protective packaging, pallet layout, and freight planning before shipment. Standard 20-foot, 40-foot, and 40-foot high-cube containers provide approximately 33.2 m³, 67.7 m³, and 76.4 m³ of internal volume. Actual usable capacity varies with container design, packaging clearance, load limits, and applicable transport regulations.

FAQS

What material information should buyers provide before requesting a casting quotation?

State the complete alloy grade, applicable standard, heat-treatment condition, and required mechanical properties. “Stainless steel” is too vague. Request chemical analysis and heat-treatment records.

Which documents help confirm the supplied material?

Ask for a material certificate, chemical analysis, and heat-treatment records. Match each document to the ordered alloy and production batch. Small wording gaps can create serious performance risks.

How should dimensional requirements be communicated?

Send a dimensioned 3D model and a controlled drawing. Mark critical dimensions clearly. Include revision numbers, datums, tolerances, measuring equipment, and inspection temperature.

Should every casting dimension use a very tight tolerance?

No. Use tighter tolerances only for sealing faces, bearing seats, and assembly datums. A 0.2 millimeter tolerance may be realistic in one area but expensive elsewhere.

How should surface finish requirements be defined?

Use measurable roughness values, such as Ra, with inspection locations. Define acceptable visual conditions, gate marks, flash removal, pits, and shot-blast texture.

What should buyers inspect on supplier samples?

Request a sample using the same alloy, geometry, and surface finish. Inspect thin walls, sharp corners, holes, and visible weld repairs. Perfect samples deserve caution.

How can buyers evaluate a supplier’s actual production capability?

Review wax injection, shell building, burnout, pouring, and finishing records. Confirm furnace size, monthly capacity, tooling resources, inspection staff, and backup equipment. A machine list is not enough.

What production controls should be confirmed before regular orders?

Ask how batches are tracked from raw material to final packing. Request dimensional data, equipment calibration records, and one corrective-action report. The answer may reveal more than polished promises.

Why is a pilot order useful?

A pilot order can reveal real yield, defect patterns, and lead times. Retained samples and documented approval points reduce later disputes. Some assumptions still survive.

Conclusion

This guide presents ten practical tips to help global buyers manage Lost wax casting projects with greater confidence. It explains the basic casting process and highlights the quality factors that influence results, including alloy selection, dimensional accuracy, tolerance control, and surface finish. Buyers will also learn how to communicate technical requirements clearly and evaluate suppliers through certifications, representative samples, equipment, workforce, and production capacity.

The article also covers the commercial and logistical aspects of purchasing castings internationally. It offers guidance on reviewing tooling charges, minimum order quantities, lead times, payment terms, and production schedules before placing an order. Finally, it emphasizes systematic inspection of finished castings, accurate documentation, secure packaging, shipping coordination, and compliance with applicable import, export, safety, and quality requirements. Together, these recommendations help buyers reduce misunderstandings, control costs, prevent delays, and build reliable long-term supply relationships.
Aria

Aria

Aria is a dedicated marketing professional with a deep passion for innovative strategies and a keen understanding of our company's product offerings. With a wealth of experience in the industry, Aria excels at crafting engaging content that highlights the unique features and benefits of our......